Commercial Epoxy Flooring: Warehouse, Kitchen and Auto Shop Floors
On 2026-10-12
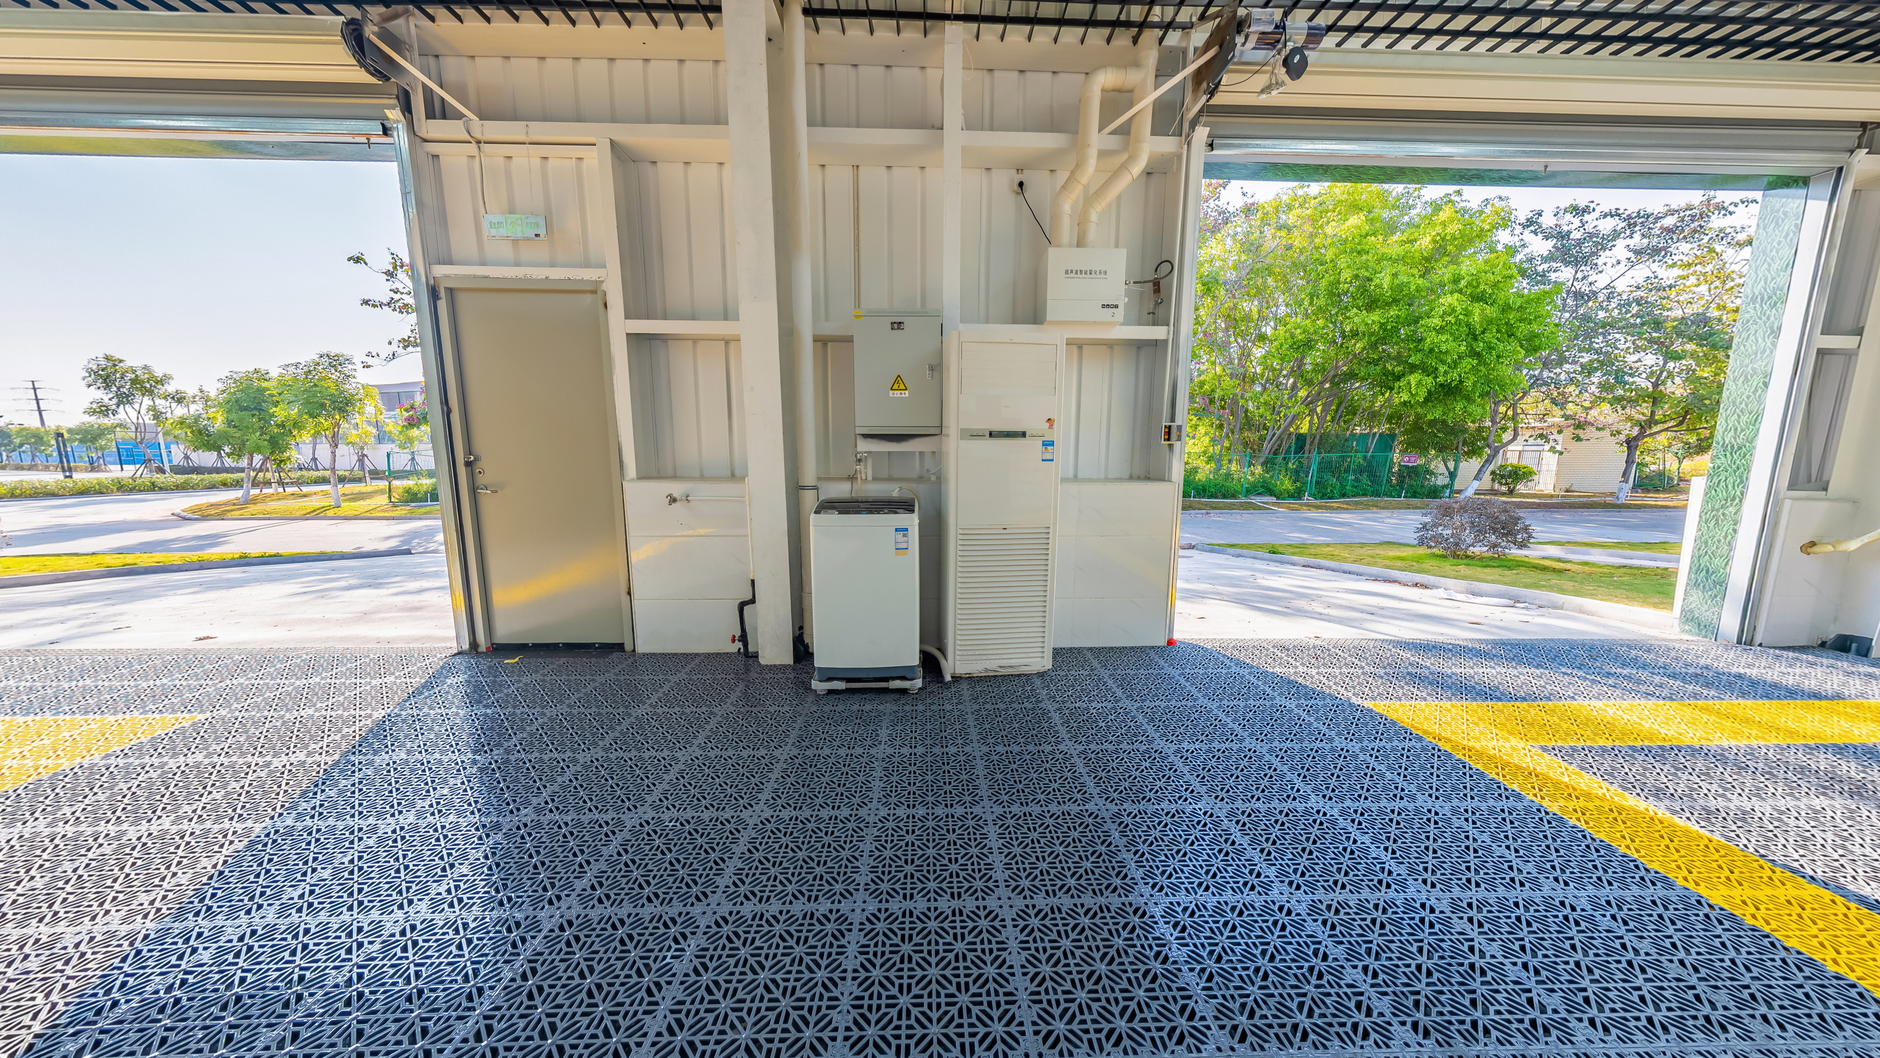
A warehouse floor and a home garage floor get sold under the same two words, and they are not the same product. They do not share a thickness, they usually do not share a resin chemistry, and they certainly do not share a failure mode. A garage coating fails when it looks tired. A distribution floor fails when a forklift turns on the spot at a dock door and peels a dinner plate sized flake off the slab, and now you have a trip hazard, an exposed patch of concrete that will dust into your product, and a repair that has to happen while the building is running.
Facility managers in Allen and across Collin County get quoted for the first thing when they asked for the second. The quotes look competitive because they are describing different floors. Reading a commercial proposal properly means knowing which questions separate the two, and almost all of them come back to load, chemistry and downtime rather than colour.
A commercial estimator should be asking what the floor does before asking what it should look like. Wheel type, chemical exposure, washdown temperature, drain locations, shift pattern. A contractor working the commercial side of this trade, such as epoxy flooring allen prime in allen, will typically want to walk the space during operating hours rather than after close, because an empty building tells you nothing about where the traffic actually concentrates.
Thickness is the argument, and it is measured in mils
Residential garage systems are commonly built somewhere between fifteen and forty mils total, a mil being one thousandth of an inch. That is a coating. It sits on the concrete, takes rubber tyres and dropped tools, and does its job.
Industrial systems start where that stops. A light duty commercial floor might be sixty to one hundred and twenty mils. A mortar system under forklift or pallet jack traffic is typically a quarter inch, and in some plants three eighths. At that point the resin is no longer a coating at all, it is a wearing surface with its own structural depth, and the difference in behaviour is not proportional to the difference in thickness. It is much larger.
The reason is how load arrives. A car tyre spreads its weight over a broad contact patch. A loaded pallet jack puts several thousand pounds through two small hard polyurethane wheels, and a forklift adds a point load plus a twisting shear force every time it steers while stationary. A thin film has nothing underneath it to distribute that. It crushes at the edge of the contact patch and then delaminates outward from the bruise.
So the first thing to establish in a proposal is a stated system thickness, in mils or in fractions of an inch, for each area of the building. A number that appears nowhere in writing is a number that will be decided by how much material is left on the truck.
Self-leveling and mortar systems do different jobs
Self-leveling epoxy is a flowable resin poured and spread to a consistent depth, usually forty to a hundred and twenty five mils. It produces a smooth, seamless, easy to clean surface and it hides minor slab irregularity because it finds its own level. It is the right answer for clean production areas, laboratory and assembly space, storage with light wheeled traffic, and anywhere hygiene and cleanability matter more than impact resistance.
A trowel applied mortar system is a different animal. Resin is mixed with graded aggregate to something like a damp sand consistency, screeded down, and power trowelled. The aggregate is what carries the load, and the resin is the binder holding it together. These are the systems specified for battery charging bays, dock aprons, heavy machining, anywhere hot or heavy objects get dropped, and any slab so worn that a flowable product would simply mirror the damage.
The practical tell in a quote is whether one system is proposed for the entire building. Most real facilities need at least two, because the receiving area and the office corridor are not doing the same work.
Commercial kitchens need urethane cement, not epoxy
This is the most consequential distinction on the food service side, and it gets missed constantly. Standard epoxy has a fairly low tolerance for thermal shock. Pour two hundred degree water onto an epoxy floor bonded to a slab at seventy degrees and the coating expands while the concrete does not. Do that nightly for a year and the bond fails, usually starting at the drains and under the dish pit where the temperature swing is worst.
Urethane cement, sometimes sold as urethane mortar or cementitious urethane, is formulated for exactly this. Its thermal expansion behaviour is much closer to concrete, so a hot washdown does not tear it off the slab. It also handles the organic acids that come out of food service, lactic acid from dairy and the sugars and fats in a production kitchen, far better than a standard epoxy does. It is usually applied at a quarter inch, it can go down on a slab that is not bone dry, and it is not as pretty as a decorative epoxy. In a kitchen that trade is obvious.
Slip resistance is not optional here either. A kitchen floor is wet, greasy and moving fast, and a smooth resin floor in that environment is a genuine hazard. Aggregate is broadcast into the system at a controlled rate to produce texture, and the specification should name the texture level, because there is a real tension between a floor that grips and a floor a mop can actually clean.
Cove base and drainage detail
A commercial kitchen floor should turn up the wall. An integral cove, typically four to six inches high, formed in the same material and radiused rather than square, removes the joint where the floor meets the wall. That joint is where water and food debris collect, and it is the first place a health inspector will look.
The same applies at every drain. The floor must be cut back, keyed into the drain, and terminated mechanically so water cannot track underneath. A resin floor that simply runs up to the edge of a drain and stops is a floor that will lift there first. Expect the proposal to say how drains and thresholds are terminated, and expect a saw cut keyway at every perimeter and doorway rather than a feathered edge.
Health department expectations vary by jurisdiction, so the useful question is not which code number applies but whether the system being proposed is one the inspector in your area routinely passes. An installer working local kitchens will know.
Auto shops, and what solvents do to a floor
An automotive shop is a chemical problem more than a load problem. Brake fluid, transmission fluid, battery acid, solvent based cleaners and the constant drip of used oil all attack a resin floor, and they do it at the point where a vehicle sits rather than uniformly. Standard epoxy handles oil and most fluids well. It is less happy with strong solvents and battery acid, which is why a service bay is usually specified with a chemically resistant topcoat and a heavier build than a showroom.
Hot tyre pickup is the other one, and it is the failure most shop owners have already seen. A vehicle driven in from a Texas summer afternoon parks on the coating with tyres well above ambient, the rubber softens the surface slightly, and when the car leaves it takes a disc of coating with it. Thickness and a properly cross linked topcoat prevent it. A thin film over inadequate preparation does not.
Showrooms and retail
A showroom floor carries almost no mechanical load and an enormous amount of visual scrutiny. The risks move from delamination to scratching, hazing under directional lighting, and yellowing where sunlight hits it through a storefront.
For these spaces the build coat matters less than the topcoat. An aliphatic urethane or polyaspartic clear resists ultraviolet light and will not amber the way a standard epoxy clear does behind west facing glass. Gloss level is worth deciding deliberately, since a high gloss floor shows every scuff and every footprint under track lighting, while a satin finish reads as more expensive in most retail settings and hides far more.
Line striping and safety zones
Once the floor is down, it can be marked, and marking a warehouse properly is cheap compared to the floor itself. Aisle boundaries, pedestrian walkways, equipment footprints, electrical panel clearance zones, battery charging areas, keep clear boxes at exits.
Two ways to do it. Tape is fast, reversible and gets peeled up by pallet jack wheels within months in a busy aisle. Coated striping, masked and sprayed or rolled into the system and then sealed under the topcoat, is permanent and will not lift because nothing sits proud of the surface. If your layout is stable, coat the lines in. If you are still moving racking, tape now and coat the lines when the layout settles.
Installing around a business that cannot close
This is usually the real constraint, and it is where most commercial jobs go wrong. Phased installation means dividing the building into zones and coating them in sequence, with saw cut terminations at each boundary so the joint between phases is deliberate rather than an accident. Racking gets shifted, one bay at a time, over several nights. It costs more in labour and it lets a warehouse keep shipping.
Fast cure chemistry is the other lever. Polyaspartic and fast cure urethane topcoats can be walked on within hours rather than overnight, and a kitchen floor in urethane cement can sometimes go down after close and take service the following evening. That speed is bought with a very short working window, which means more crew on site and less tolerance for anything going wrong, so it is a scheduling decision rather than a free upgrade.
What a commercial specification should contain
The proposal should name, per area of the building: the system and its total thickness, the surface preparation method and the resulting profile, how cracks and joints are treated, the primer, the build coat, the topcoat and its ultraviolet stability, the slip resistance additive and its rate, how the floor terminates at walls and drains, and the cure times before foot traffic, before wheeled traffic and before chemical exposure. Those three cure times are different numbers, and a proposal that lists only one is hiding the long one.
Warranty language deserves the same reading. A material warranty covers the resin and is largely the manufacturer's promise. A workmanship warranty covers the installation, which is where almost all failures originate, and it is the one that should carry a stated duration and a named remedy. Ask what voids it. Forklift tyre type, washdown chemistry and temperature, and cleaning products are all common exclusions, and it is much better to learn that your sanitiser is excluded before the floor goes down than during a claim.